Table of Contents
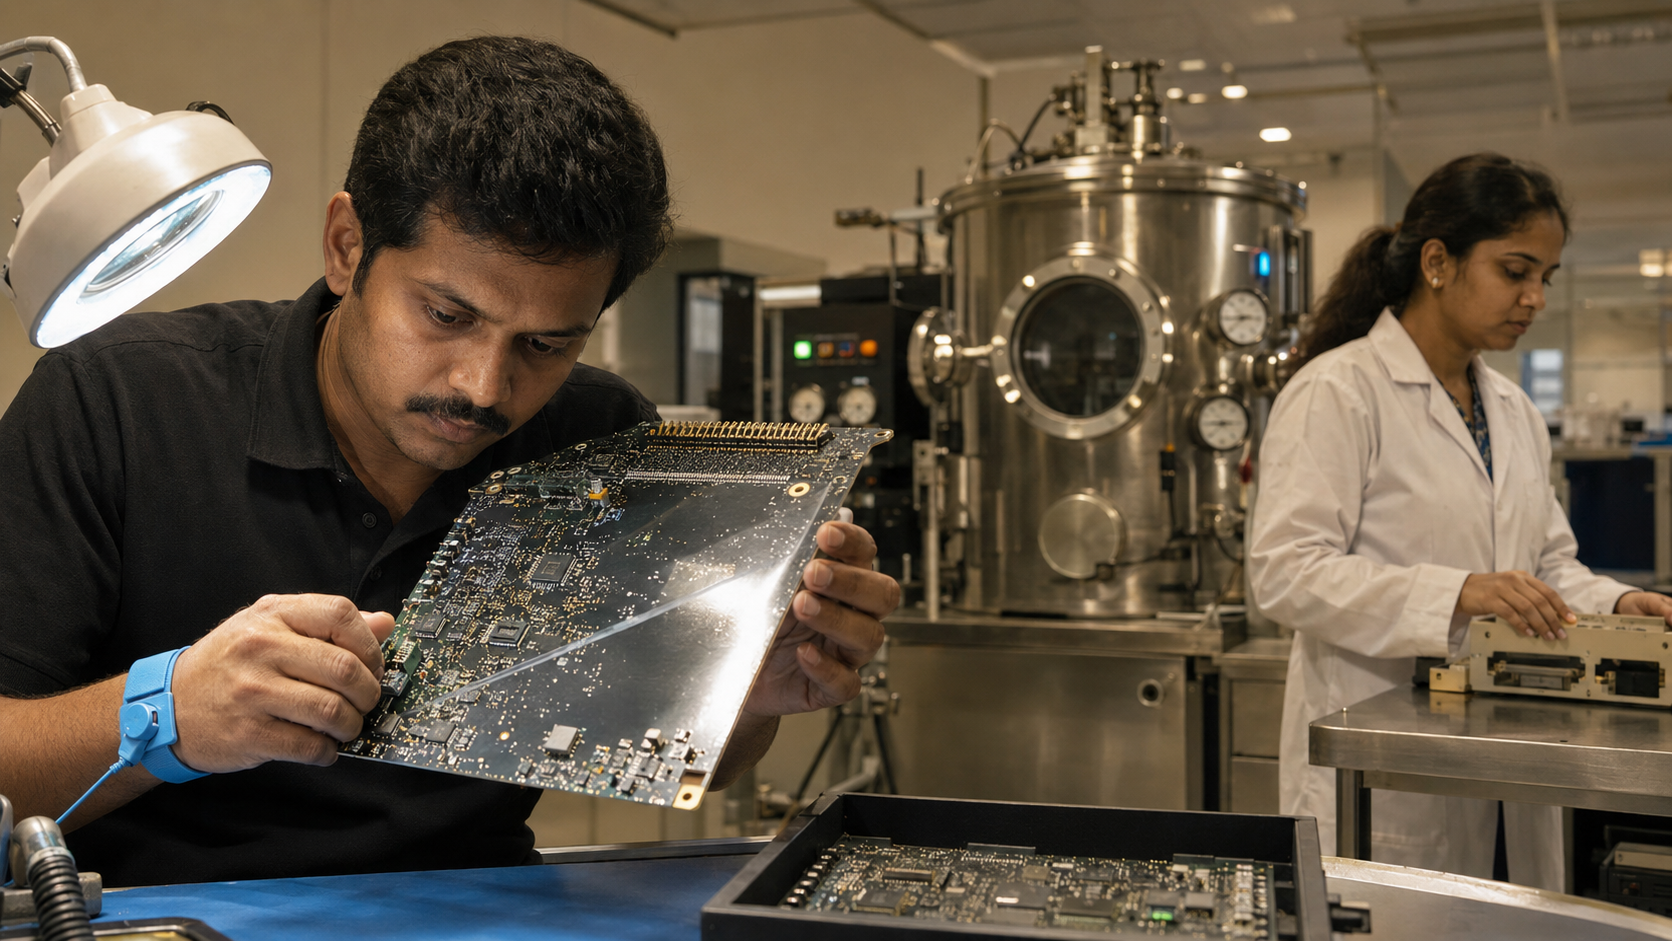
A printed circuit board sits between three coating quotes: one at half the price of the other two, one that arrives with no number at all, and one padded with specifications nobody asked for. This is the ordinary experience of anyone sourcing coating for the first time, and it is exactly why parylene coating cost confuses so many buyers before they place an order. Parylene is applied inside a sealed vacuum chamber through chemical vapor deposition, a process where price moves with chemistry, thickness, and what has to stay uncoated, not with a flat rate per square foot.
Understanding those variables before requesting a quote is what separates a buyer who can evaluate three different numbers from one who is stuck guessing which vendor overpriced the job. This guide breaks down what actually drives parylene coating cost, what a fair quote accounts for, and what that looks like for manufacturers sourcing coating out of India. It is written for the engineer or procurement lead comparing quotes for the first time, and it deliberately skips the chemistry lecture in favor of the questions that actually change the number on the invoice.
What Actually Determines Parylene Coating Cost

Parylene coating cost is set by four interacting variables: the Parylene type selected, the required coating thickness, the complexity of the masking needed to protect connectors and contact points, and how many parts fit into a single vacuum chamber run. These are treated as the primary technical inputs behind every serious quote, not a flat per-unit rate.
No two of these variables move independently. A thicker coating on a simple, easily masked part can cost less than a thin coating on a component with a dozen connectors that all need protecting. This is why a vendor asks for a drawing before quoting parylene coating cost, not just a part count.
| Cost Driver | What It Affects | Practical Note |
|---|---|---|
| Parylene type | Raw material (dimer) cost per run | C and N are lower cost; HT and specialty types cost more |
| Coating thickness | Dimer consumed, chamber time | Thicker specs consume more dimer per part |
| Masking complexity | Labor hours before and after coating | Connectors, threads, and moving parts add time |
| Chamber load (batch size) | Cost distributed per part | More parts per run lowers per-unit cost |
HZO’s published guidance on budgetary quotes for parylene coatings treats part dimensions, masking requirements, and annual production volume as the primary technical inputs behind every serious estimate. A vendor who skips these questions and jumps straight to a number is usually guessing.
Chamber time itself is close to a fixed cost per run, regardless of how full the chamber is. That fact explains most of the confusing price variation between vendors: a facility running near-empty chambers recovers fixed cost across fewer parts, while a fully booked facility spreads it further and quotes lower. Neither number is wrong, they reflect utilization, not honesty.
Parylene Type: Why C, N, and HT Are Priced Differently
Not every Parylene variant costs the same to apply, and the type selected changes the raw material bill before labor even enters the calculation. Parylene C and Parylene N are the most common and the most economical dimers. Specialty variants such as Parylene HT cost more because they deliver higher heat resistance and better UV stability.
| Type | Relative Material Cost | Typical Use Case |
|---|---|---|
| Parylene C | Lower | General PCB and electronics protection |
| Parylene N | Lower | High-frequency and low-dielectric applications |
| Parylene HT | Higher | High-temperature, UV-exposed, aerospace-grade parts |
Specialty Coating Systems, a manufacturer with decades of Parylene production experience, notes that standard dimer runs close to $200 per pound for common types, while specialty variants command a premium for the added performance. That figure is a US benchmark, not an India-specific rate, but it explains why a spec sheet calling for Parylene HT without a genuine thermal requirement inflates cost for no functional gain.
The type decision should follow from the application, not the other way around. A consumer electronics assembly operating well inside normal ambient temperature has no functional reason to specify a heat-resistant variant, and doing so simply moves the raw material line item up without adding protection the part will ever use. A defense or under-hood automotive component facing genuine thermal cycling is the opposite case, where the added parylene coating cost of a specialty dimer buys real reliability margin rather than an unused spec.
Coating Thickness and Its Effect on Price

Thickness is the second lever on parylene coating cost, and it works in a straightforward direction: a thicker coating consumes more dimer per part, which raises the material portion of the bill. Most electronics applications need somewhere between 0.5 and 25 microns, and specifying the minimum thickness that meets the reliability requirement is one of the few parylene coating cost levers fully in the buyer’s control.
Over-specifying thickness is a common and avoidable mistake. A design engineer who copies a thickness value from a previous project without recalculating for the new part’s actual exposure risk can end up paying for protection the application does not need.
Push Digital’s Parylene coating service works from the part’s actual environmental exposure, not a default number, when recommending thickness, which keeps parylene coating cost tied to the real reliability requirement rather than a copied specification.
Thickness also interacts with the part’s tolerance stack. A part with tight clearances around connectors or moving components can only accept so much added thickness before the coating interferes with fit, which sometimes forces a thinner spec than the reliability target alone suggests. That constraint is worth raising with the vendor early, since it changes both the coating approach and the final parylene coating cost.
Masking Complexity: The Most Underestimated Cost Driver
Masking is consistently the most underestimated line item in a parylene coating quote, because buyers picture the coating step and forget the preparation step that precedes it. Every surface that must stay bare, a connector, a ground pad, a threaded fastener, has to be individually sealed before the part enters the chamber, and that sealing is manual labor.
Parts commonly requiring careful masking include:
- Board-to-board and cable connectors
- Threaded fasteners and mounting points
- Ground pads and test points
- Moving mechanical components
Picture a connector-heavy sensor assembly quoted as a simple coating job. Once the vendor counts fourteen individual masking points across the connector, the mounting bracket, and the test pads, the labor hours double, and the quote the buyer expected turns out to be roughly half the real number. Because Parylene is deposited from a gas rather than sprayed, masking has to be genuinely airtight, which is why this step, not the coating itself, is usually where a quote goes over budget.
Design choices made months before the vendor is contacted determine how bad this problem gets. A connector placed flush against a housing wall is harder to mask than one with clearance around it, and a reused component library can carry forward a masking problem nobody has revisited. Reviewing masking implications before finalizing a design, rather than after the first quote comes back high, is one of the few genuinely free ways to control parylene coating cost.
Batch Volume and Chamber Load Economics

Batch size changes the economics of parylene coating cost more than almost any other variable, because each coating run has a largely fixed cost regardless of how many parts sit inside the chamber. A vendor coating five parts and a vendor coating five hundred parts in an equivalent chamber pay close to the same run cost, so the per-unit price falls sharply as batch size grows.
This is why a single prototype coating run often looks expensive on a per-part basis even from a fair vendor. The fixed chamber cost is being divided across one part instead of hundreds. Manufacturers moving from prototype to production volume should expect a meaningfully lower per-unit quote once batch size increases, not because the vendor discounted the work, but because the fixed cost is now spread further.
Matching batch size to chamber capacity, rather than running partially filled chambers, is the single most effective lever a manufacturer has for controlling recurring parylene coating cost across a production run.
This has a direct scheduling implication. A vendor may hold a partially filled chamber for a few days waiting to combine a smaller order with another client’s parts, which lowers the per-unit price but adds lead time, or run it immediately at a higher per-unit rate. Buyers with flexible timelines and buyers who need parts back the same week are effectively negotiating two different variables, and being explicit about which one matters more usually gets a better outcome than pushing on price alone.
Parylene Coating Cost in the Indian Manufacturing Context
India’s parylene coating market is still maturing relative to the US and European supply base, and that affects parylene coating cost in a specific way: dimer is largely imported, so raw material pricing tracks global rates plus logistics, while coating labor and chamber time are priced domestically. Buyers should expect quotes structured around imported material cost and local processing cost as two separate line items.
Push Digital has been building brands out of Chennai for more than 25 years. That same manufacturing-region experience shapes how coating and production projects are scoped for Tamil Nadu and India-based clients, including production and coating work in Push Digital’s portfolio.
Common project categories seeking parylene coating in India include EV electronics and battery management sensors, medical device components requiring biocompatible protection, and defense or aerospace hardware needing MIL-spec level moisture resistance. Each category carries a different masking and thickness profile, which is why a generic per-square-inch rate rarely applies across sectors, and why an accurate quote still requires a real part drawing rather than a category assumption.
Lead time is the practical consequence of import dependency that buyers tend to overlook. A dimer shipment delay does not just push out the coating date, it pushes out the assembly line waiting on that coated part. Manufacturers on tight production calendars should raise dimer lead time with the vendor early, not treat it as a variable that only surfaces when something goes wrong.
Parylene vs Other Conformal Coatings: Is the Cost Worth It

Parylene sits at the expensive end of the conformal coating spectrum compared with acrylics, epoxies, silicones, and urethanes, and that comparison is where the “is it worth it” question actually gets decided. Parylene delivers protection at roughly half the thickness of conventional acrylic or epoxy coatings, which matters directly for space-constrained electronics.
The real comparison is not upfront coating price against upfront coating price. It is total cost of ownership: a cheaper acrylic coating that lets moisture through under field conditions can trigger warranty claims and field failures that cost far more than the coating saved. Parylene’s pinhole-free, uniform barrier is why high-reliability sectors accept the higher parylene coating cost as a trade against downstream failure cost.
Push Digital also runs electroluminescent printing services alongside Parylene coating for clients whose products combine illuminated components with moisture-sensitive electronics, since the two specialty coating and finishing processes are frequently specified on the same product.
A silicone or urethane coating carries a lower upfront price than parylene coating cost typically runs, which makes it the right call for lower-reliability consumer products where a field failure is inconvenient rather than costly. Parylene earns its higher price specifically where a coating failure has consequences beyond a single unit, a medical implant, an automotive safety sensor, or a defense system where field service is not a simple option.
What to Ask a Vendor Before You Request a Quote
A useful parylene coating cost quote starts with the buyer supplying the right information, not the vendor guessing at it. Vendors who ask detailed questions upfront are generally the ones who deliver quotes that hold once the actual work begins, rather than revised numbers after masking complexity surfaces mid-project.
Before requesting a quote, be ready to answer:
- What is the exact part geometry and which surfaces must remain uncoated
- What minimum coating thickness meets the application’s reliability requirement
- What is the expected annual or batch volume
- What environmental conditions will the part face in service
- Which Parylene type is required, and is that requirement based on an actual spec or a copied default
A vendor who can quote accurately without asking most of these questions is either working from an inflated flat rate or has not fully scoped the job.
The same logic runs in both directions. A buyer who cannot answer these questions when asked is not ready to compare quotes yet, and pushing forward anyway just produces numbers that cannot be compared against each other, since each vendor will have filled the gaps with different assumptions. Getting these five answers settled internally before the first vendor call is the fastest way to keep the eventual parylene coating cost quotes apples to apples.
Conclusion
Parylene coating cost is not a mystery once the four real variables, type, thickness, masking, and batch volume, are on the table. A buyer who walks into a vendor conversation with a part drawing, a thickness requirement backed by an actual reliability need, and a realistic volume estimate will get quotes that are comparable to each other, rather than three numbers that seem to describe three different jobs.
The one action worth taking this week is pulling together those specifics before the next quote request goes out, since that alone resolves most of the confusion buyers run into on this topic. For manufacturers weighing parylene coating against other protection methods for an upcoming production run, Push Digital’s technical team can walk through the part drawing and the real cost drivers before the first vendor quote comes in. A well-scoped drawing, not a lower asking price, is what actually keeps parylene coating cost predictable across a production run.
Frequently Asked Questions
What determines parylene coating cost?
Parylene type, coating thickness, masking complexity, and chamber batch size determine parylene coating cost. Masking is the most frequently underestimated of the four, since it is manual labor performed before the coating run begins.
Why does parylene coating cost not have a fixed price per unit?
Because each part’s masking requirements and chamber load differ, a fixed per-unit rate would misprice most jobs. Vendors quote from a drawing and volume estimate rather than a flat catalogue price.
Is Parylene C or Parylene N cheaper?
Both are among the lower-cost, most common dimer types, priced similarly to each other. Specialty types like Parylene HT cost more due to added heat and UV resistance.
Does batch size affect the cost per component?
Yes, significantly. Chamber runs carry a largely fixed cost, so spreading that cost across more parts per batch lowers the per-unit price.
How does masking complexity change the price?
Every surface that must stay uncoated needs manual sealing before the part enters the chamber. More connectors, threads, or moving parts mean more labor hours.
Is parylene coating worth the cost compared to acrylic or epoxy coating?
For high-reliability applications, usually yes. Parylene’s thinner, pinhole-free barrier reduces field failure risk, which often outweighs the higher upfront coating cost.
What information does a vendor need to give an accurate quote?
Part geometry, required thickness, masking points, batch volume, and service environment. A vendor quoting without this information is estimating, not calculating.